Description
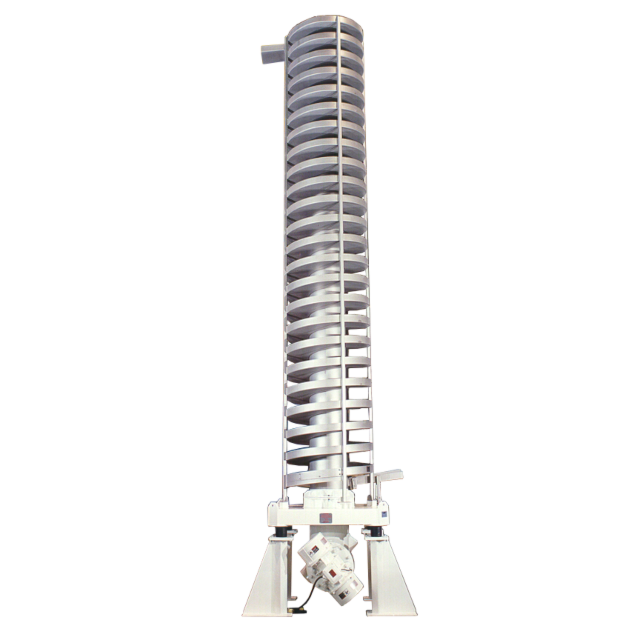
Vibrating spiral elevators transport bulk solid products upwards to accommodate space constraints and production line layouts, but they also effectively process the product during transport.
Perforations can be incorporated into the central tower to blow air through the product bed, and sheathed spirals can provide indirect heat transfer via steam, oil, or water.
Carrier spiral elevators are custom-built in various sizes (up to over 3 m in diameter and 15 m in height), for light or heavy-duty applications, high temperatures, and sanitary design. They can be enclosed to protect the product environment or ensure operator safety.
The retention time can be adjusted for even greater control over the finished product conditions. Spiral elevators are commonly used in the food and pharmaceutical industries, as well as for processing rubber, plastics, and other polymers.
The French exhibition dedicated to
Industrial bulk material handling
114 rue de Calonges
47440 Casseneuil