Description
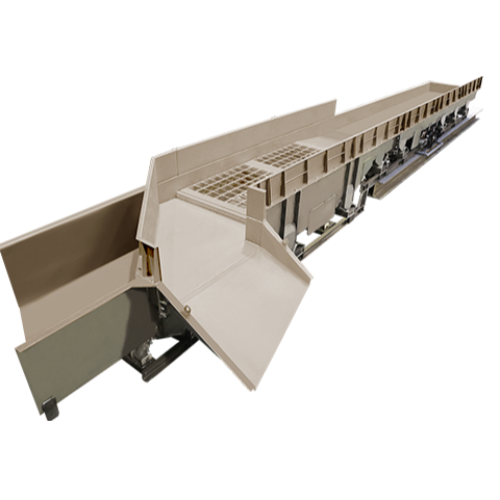
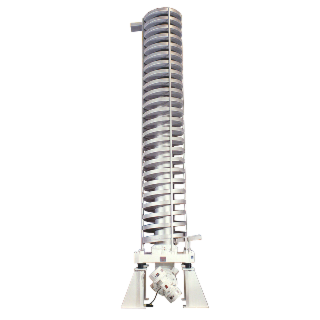
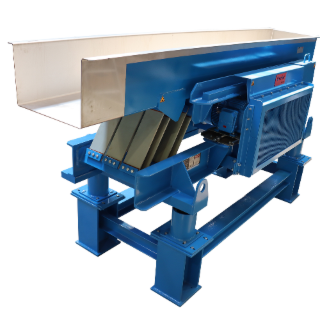
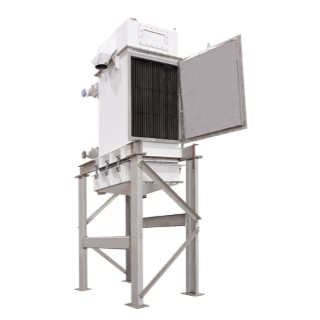
Carrier vibrating conveyors enable the highly controlled transport of bulk materials and are custom-designed to handle all types of solid products, ranging from the lightest and most delicate to the heaviest and most abrasive.
Carrier pioneered the use of natural frequency as a "drive component" for vibrating equipment: the drive mechanism is tuned to resonate with the spring system supporting the conveyor trough. Once in motion, drive energy is "stored" and released by the springs, keeping the conveyor in constant motion and significantly reducing energy consumption. The springs are evenly distributed along the conveyor to prevent stress and the risk of breakage.
Thanks to this technology, conveyors exceeding 90 meters in length can operate using just a single motor!
In addition to energy efficiency, vibrating technology offers benefits such as reduced equipment and product degradation, as no moving parts come into contact with the material being conveyed.
This also allows for the use of various trough materials to suit harsh environments, high temperatures, heavy loads, or sanitary requirements (for food, chemical, or pharmaceutical products). The trough can even be designed for easy replacement.
Vibrating conveyors can also be multifunctional, incorporating screening zones, metal-free sections, or sorting/distribution discharge points.
The French exhibition dedicated to
Industrial bulk material handling
114 rue de Calonges
47440 Casseneuil